I want to set tool 1 and reference the other tools from there, sounds
like what you are doing too.  So, after setting tool 1, I next find the
offset for tool 2.  Are the offsets entered by editing the tbl file with
a text editor?  I looked a the g-code reference but when I clicked on
G43, it looked for an internet connection, that computer isn't connected
to the internet.  I was wondering what the X and Z did from G43, are
they the offset amounts or are they move commands?
Thanks!

Roger Neal


----- Original Message -----
From: "Chris Radek" <[EMAIL PROTECTED]>
To: "Enhanced Machine Controller (EMC)"
<[email protected]>
Sent: Tuesday, June 26, 2007 9:06 PM
Subject: Re: [Emc-users] Lathe ? Using Tool Offsets


> On Tue, Jun 26, 2007 at 07:13:36PM -0500, RogerN wrote:
>> Or maybe my question should be how do you set up the TLO table
>> for lathes?
>>
>> Sorry for such a basic question but I'm new to EMC2 and lathes and
>> haven't been able to find a procedure for this in the documentation
>> or
>> through google.
>
> First make sure you have a lathe format tool table.  There are some
> examples in CVS - here's one:
>
> <http://cvs.linuxcnc.org/cgi-bin/cvsweb.cgi/emc2/configs/lathe-pluto/emc.tbl?rev=1.1>
>
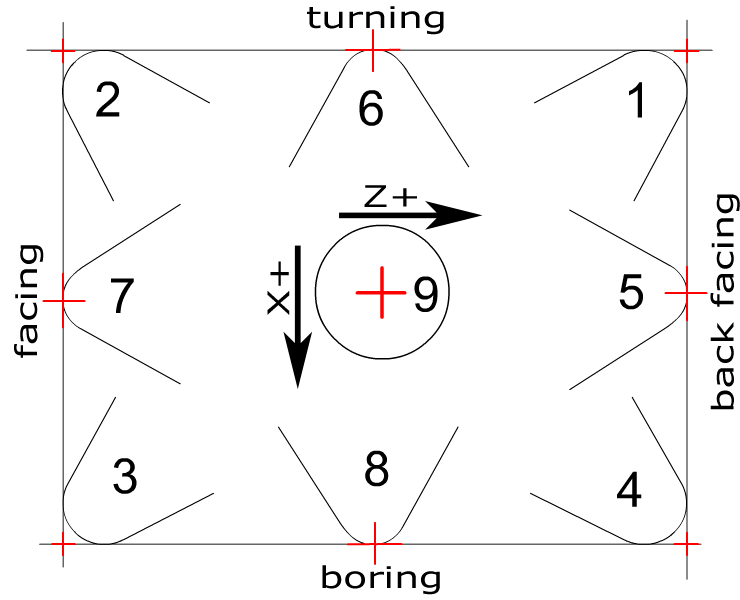
> You'll want to set diameter (which is the diameter of the radiused
> tool tip), orientation, and the two offsets for each tool.  The angles
> are nice for seeing the tool shape in AXIS but are otherwise unused so
> far.  The diameter and orientations are required for G41/G42 and of
> course the offsets are required for G43.
>
> Orientations:
>
> <http://wiki.linuxcnc.org/uploads/cutting_orientation2.png>
>
> How you set your offsets is a personal preference thing - I'm sure
> people do it differently.  I like to set them relative to a reference
> tool, which in my case is orientation 2 (left cutting turning tool).
> I use that because I can both turn and face with it to do my touch
> offs without worrying about G43.  You could also measure in both
> directions from your tool holder etc (like measuring down from the
> spindle on a mill).
>
> Whether you get the measurements by turning material and measuring its
> diameter or by measuring the tools in their holders or whatever is up
> to you - you just need to somehow determine the offsets.  This
> sometimes takes some creativity.  To get a threading tool's offset
> exactly right, you'll probably have to cut a thread and measure it
> with thread wires.  John K and I entertained (ha) a large group of
> folks at cnc workshop trying to do this.
>
> If you load that tool table I linked above and change tools in AXIS
> you'll get a good feeling of the meaning of the angles and
> orientations.
>
> Good luck - this is intricate setup but it's rewarding to be able
> to change tools and not worry about it once it's done.
>
> Chris
>
>
> -------------------------------------------------------------------------
> This SF.net email is sponsored by DB2 Express
> Download DB2 Express C - the FREE version of DB2 express and take
> control of your XML. No limits. Just data. Click to get it now.
> http://sourceforge.net/powerbar/db2/
> _______________________________________________
> Emc-users mailing list
> [email protected]
> https://lists.sourceforge.net/lists/listinfo/emc-users


-------------------------------------------------------------------------
This SF.net email is sponsored by DB2 Express
Download DB2 Express C - the FREE version of DB2 express and take
control of your XML. No limits. Just data. Click to get it now.
http://sourceforge.net/powerbar/db2/
_______________________________________________
Emc-users mailing list
[email protected]
https://lists.sourceforge.net/lists/listinfo/emc-users